Guides
Evergreen how-tos and buyer's guides, written in plain English with the trade-offs that actually matter.
-
Guides
Oomwoo: An Open-Source, Fully Offline Robot Vacuum You 3D Print and Build Yourself
Maker's Pet is building Oomwoo, an Apache 2.0 3D-printed robot vacuum with Raspberry Pi, LiDAR, and ROS 2/Nav2 that runs entirely offline to dodge the cloud-hijacking bugs found in commercial vacuums.
-
Guides
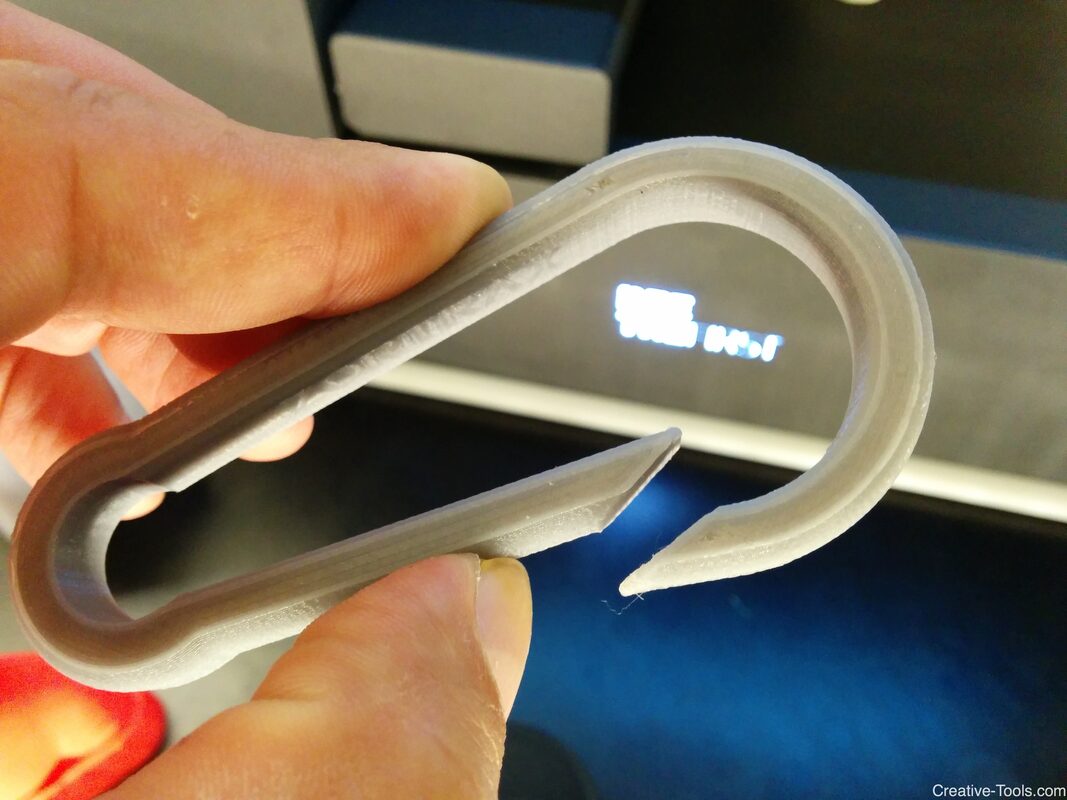
Snap Fit Design for 3D Printing: Deflection Math, Tolerances, and Material Tradeoffs
Cantilever and annular snap fits are deceptively simple mechanisms that FDM printers struggle to reproduce reliably. Here is the geometry, deflection math, clearance strategy, and material selection logic to get them right on the first print.
-
Guides
Multi-Material FDM in 2026: Why Architecture Matters More Than You Think
Choosing a multi-material printer is really a choice between three distinct hardware architectures, each with fundamentally different tradeoffs in purge waste, contamination risk, and temperature compatibility -- and the wrong choice for your materials can make certain prints impossible.
-
Guides
Manual Color Swaps Without an AMS: G-Code Pause Commands in PrusaSlicer, OrcaSlicer, and Bambu Studio
Multi-color printing without a filament changer is entirely achievable using M600 and pause-at-layer commands. The slicer implementations differ in important ways, and getting the G-code sequencing wrong produces failed swaps, ooze blobs, or color bleed that contaminates the swap layer.
-
Guides
The Science of UV Post-Curing Resin Prints: Wavelength, Time, and Temperature
Post-curing is the most underestimated variable in MSLA and DLP resin printing. Get the wavelength, timing, and temperature wrong and your parts will be brittle, tacky, or dimensionally unstable regardless of how well they printed.
-
Guides
Variable Layer Height: How Adaptive Slicing Gets Better Surface Quality Without the Time Penalty
Adaptive or variable layer height lets slicers use thin layers where they matter and thick layers where they don't. The result is better surface quality at nearly the same print time.
-
Guides
Threading 3D Prints: Printed Threads, Heat-Set Inserts, and Captured Nuts
Bolting 3D printed parts together reliably requires understanding when printed threads work, when heat-set inserts are worth it, and when a captured nut is the right call.
-
Guides
Resin Printing Safety: Ventilation, PPE, and Proper Disposal — What You Actually Need
Photopolymer resin contains skin sensitizers and volatile acrylate monomers. Setting up a safe workspace isn't optional — here's exactly what's required and why.
-
Guides
Living Hinges and Flex Joints: Designing Bendable Features Directly Into FDM Prints
A living hinge folds thousands of times without a fastener. In FDM, making it work requires specific geometry, the right material, and a print orientation that isn't obvious.
-
Guides
Designing and Printing Watertight Parts: Vases, Containers, and Plumbing Fittings
FDM prints aren't watertight by default. Layer gaps, infill voids, and perimeter seams all leak. Here's how to close them — in the slicer, the design, and post-processing.
-
Guides
First-Time 3D Printer Setup: From Unboxing to First Successful Print
New printer, blank slate. The gap between unboxing and a clean first print is narrower than it used to be — but getting there still requires understanding a few non-obvious steps.
-
Guides
Ironing in FDM: The Slicer Setting That Makes Flat Surfaces Glass-Smooth
Ironing passes a nearly-dry nozzle over the top layer after it's printed, remelting the surface into a flat, glossy finish. Here's how it works and when to use it.